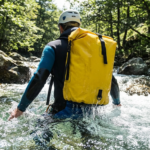





Outdoor‑Rucksäcke sind einer Kombination aus mechanischer Belastung und wechselnden Witterungsbedingungen ausgesetzt. Beim Wandern, Klettern und bei mehrtägigen Expeditionen kann das Gewebe an rauem Gestein scheuern, hohe Lasten tragen, starkem Regen ausgesetzt sein und während des Transports wiederholt gefaltet werden. Diese Bedingungen stellen hohe Anforderungen sowohl an die Textilstruktur als auch an die wasserdichte Schicht. Für Hersteller bedeutet die Auswahl eines geeigneten Materials mehr als nur die Wahl eines Gewebes mit hohem Denier‑Wert oder einer wasserdichten Oberfläche.
TPU‑beschichtetes Nylongewebe ist eine Option für Outdoor‑Ausrüstung, die eine Kombination aus Wasserbeständigkeit, mechanischer Festigkeit und überschaubarem Gewicht erfordert. Durch die Kombination eines gewebten Nylon‑Substrats mit einer Schicht aus thermoplastischem Polyurethan können Hersteller Verbundmaterialien entwickeln, die sich für wasserdichte Rucksäcke, Expeditions‑Duffelbags, Ausrüstungstaschen und andere anspruchsvolle Outdoor‑Produkte eignen.
Die endgültige Leistung hängt von der Nylonkonstruktion, der Struktur der TPU‑Beschichtung, der Qualität der Laminierung, der Verbindungsmethode sowie dem Design der fertigen Tasche ab. Ein Material, das für einen leichten Tagesrucksack gut geeignet ist, bietet möglicherweise nicht das gleiche Gleichgewicht aus Flexibilität und struktureller Unterstützung, das ein großer Expeditionsrucksack benötigt.
Für Produktentwickler und Beschaffungsteams sollte der Auswahlprozess mit der vorgesehenen Anwendung beginnen und anschließend eine Vergleichsanalyse der Gewebespezifikationen und Fertigungsanforderungen durchgeführt werden. Dieser Ansatz hilft zu bestimmen, ob eine bestimmte TPU‑beschichtete Nylonkonstruktion die praktischen Anforderungen des Endprodukts erfüllen kann.
Was macht TPU‑beschichtetes Nylongewebe für Outdoor‑Rucksäcke geeignet?
Ein Rucksackgewebe muss gleichzeitig mehrere Funktionen erfüllen. Es muss äußere Feuchtigkeit abweisen, Abrieb standhalten, die über die Taschenstruktur übertragenen Lasten tragen und beim Zuschneiden sowie bei der Montage verarbeitbar bleiben. Die wasserdichte Schicht muss zudem während der gesamten erwarteten Lebensdauer des Produkts fest am Textilsubstrat haften.
TPU‑beschichtetes Nylongewebe kombiniert zwei Materialkomponenten mit unterschiedlichen Funktionen.
Das gewebte Nylon‑Grundgewebe sorgt für Zugfestigkeit, Reißfestigkeit und Dimensionsstabilität. Seine Leistung hängt von den Garncharakteristika, der Webkonstruktion, der Gewebedichte und der Oberflächenveredelung ab. Die TPU‑Schicht bildet die funktionelle Oberfläche, die für die Wasserbeständigkeit erforderlich ist, und trägt zur Flexibilität und Haltbarkeit des Verbundmaterials bei.
Diese Konstruktion bietet Herstellern mehr Möglichkeiten bei der Entwicklung von Outdoor‑Produkten für verschiedene Gewichtsklassen und Einsatzumgebungen. Das Gewebe kann entsprechend dem erforderlichen Gleichgewicht zwischen Tragfähigkeit, Oberflächenbeständigkeit, Flexibilität und Transportfähigkeit ausgewählt werden.
Wasserdichter Schutz bei wechselhaften Wetterbedingungen
Regenschutz ist ein Hauptkriterium für Rucksäcke, die auf offenen Pfaden und bei längeren Touren eingesetzt werden. Feuchtigkeit, die über die Hauptflächen eindringt, kann Kleidung, Schlafausrüstung, Lebensmittelverpackungen und elektronische Zubehörteile durchnässen. Ein wasserdichtes Material hilft, dieses Risiko zu reduzieren, wenn es in eine entsprechend konstruierte Tasche integriert wird.
Die TPU‑Schicht bildet eine Barriere über dem Textilsubstrat. Allerdings hängt die Wasserdichtigkeit des fertigen Rucksacks auch von Nähten, Verschlüssen, Reißverschlüssen, Befestigungspunkten und weiteren Konstruktionsdetails ab.
Eine beschichtete Fläche macht das Gesamtprodukt nicht automatisch wasserdicht. Wasser kann weiterhin durch Nadelöcher, schlecht versiegelte Nähte, Reißverschlussöffnungen oder beschädigte Stellen eindringen. Hersteller sollten das gesamte Taschendesign bewerten und geeignete Konstruktionsmethoden wählen, um das gewünschte Maß an Wasserschutz zu erreichen.
Mechanische Unterstützung unter Last
Rucksäcke übertragen das Gewicht über ihre Seitenwände, den Boden, die Schultergurte, die Griffe und die Befestigungspunkte. Diese Bereiche sind während des Gebrauchs unterschiedlichen Belastungen ausgesetzt.
Die Bodenplatte kann auf unebenem Untergrund aufliegen, während die Verbindungen der Schultergurte konzentrierten Zugkräften ausgesetzt sind. Seitenteile können durch dicht gepackte Ausrüstung zusammengedrückt werden, und Außentaschen können wiederholt an umliegenden Objekten scheuern.
Das gewebte Nylon‑Substrat trägt zur mechanischen Leistung des Verbundmaterials bei. Dennoch sollte die Festigkeit des Gewebes nicht als Ersatz für angemessene Verstärkungen und eine tragfähige Konstruktion betrachtet werden. Ein gut ausgewähltes Material muss mit dem Muster der Tasche, der Nahtanordnung, der Naht- oder Schweißmethode sowie der Verstärkungsstruktur harmonieren.
Wie sollten Käufer 420D‑ und 840D‑TPU‑beschichtetes Nylon vergleichen?
Denier ist ein nützlicher Referenzwert beim Vergleich von Nylongeweben, sollte jedoch nicht der einzige Faktor bei der Auswahl von Rucksackmaterial sein. Der Denier‑Wert gibt die lineare Dichte des Garns an, misst jedoch nicht direkt die Abriebbeständigkeit, Reißfestigkeit oder Wasserdichtigkeit des fertigen Gewebes.
Für Hersteller von Outdoor‑Ausrüstung können 420D‑ und 840D‑Nylonkonstruktionen unterschiedliche Ausgangspunkte für die Produktentwicklung darstellen. Ihre Eignung hängt von der vollständigen Spezifikation des Verbundmaterials und der beabsichtigten Nutzung der Tasche ab.
Wann ist 420D‑TPU‑beschichtetes Nylon geeignet?
420D‑TPU‑beschichtetes Nylon kann für Rucksäcke und Ausrüstungstaschen in Betracht gezogen werden, die ein Gleichgewicht zwischen struktureller Leistung und einem überschaubaren Materialgewicht benötigen.
Mögliche Anwendungen umfassen allgemeine Wander‑Rucksäcke, Reisetaschen, Outdoor‑Organizer sowie ausgewählte Einsätze in größeren Taschen. Dort, wo das Produkt relativ flexibel bleiben soll, kann eine geeignete 420D‑Konstruktion eine praktische Alternative zu schwereren Textilstrukturen bieten.
Das tatsächliche Gewicht des fertigen Verbundmaterials hängt vom Nylongewebe, dem Gewicht der TPU‑Beschichtung und der Laminierungskonstruktion ab. Zwei als 420D beschriebene Materialien können sich in Gesamtmasse, Flexibilität, Dicke und mechanischer Leistung erheblich unterscheiden.
Hersteller sollten daher die vollständige technische Spezifikation anfordern und repräsentative Proben prüfen, bevor sie ein Design finalisieren.
Wo passt 840D‑TPU‑beschichtetes Nylon?
840D‑TPU‑beschichtetes Nylon kann für Produkte in Betracht gezogen werden, bei denen zusätzliche Textilsubstanz und strukturelle Unterstützung Priorität haben. Mögliche Anwendungen umfassen schwere Duffelbags, Expeditions‑Ausrüstungstaschen, verstärkte Rucksackböden und andere Produkte, die anspruchsvollen Handhabungsbedingungen ausgesetzt sind.
Eine höhere Denier‑Konstruktion garantiert nicht automatisch bessere Leistungen in jeder Kategorie. Die Abriebbeständigkeit hängt ebenfalls von der Garnqualität, der Webstruktur, der Beschichtungsformulierung und den Oberflächeneigenschaften ab. Reißfestigkeit und Durchstoßfestigkeit erfordern separate Betrachtungen, da sie unterschiedliche Versagensmechanismen beschreiben.
Schwerere Konstruktionen können zudem die Flexibilität, das Gesamtgewicht des Produkts, das Packvolumen und das Fertigungsverhalten beeinflussen. Produktgestalter sollten diese Kompromisse gegen die tatsächlich zu erwartenden Lasten und Umweltbedingungen abwägen.
Ein praktischer Vergleich für die Produktentwicklung
| Auswahlkriterium | 420D‑TPU‑beschichtetes Nylon | 840D‑TPU‑beschichtetes Nylon |
|---|---|---|
| Typische Designrichtung | Ausgeglichenes Gewicht und Haltbarkeit | Größere Materialsubstanz und strukturelle Unterstützung |
| Mögliche Anwendungen | Wander‑Rucksäcke, Reisetaschen, Organizer | Expeditions‑Duffelbags, schwere Packs, verstärkte Einsätze |
| Gewichtsüberlegungen | Kann leichtere Produktkonstruktion unterstützen | Kann das Gesamtgewicht des Verbundmaterials erhöhen, je nach Spezifikation |
| Flexibilität | Hängt von Beschichtung und Gewebekonstruktion ab | Hängt von Garn, Webart, Beschichtung und Oberflächenveredelung ab |
| Erforderliche Überprüfung | Zug-, Reiß-, Abrieb- und Wasserdichtigkeitstests | Dieselben Tests, mit besonderer Berücksichtigung der vorgesehenen Lasten und Verschleißbedingungen |
This comparison is a general selection framework rather than a guarantee of performance. The final choice should be based on measured properties of the actual fabric supplied by the manufacturer.
Which Fabric Properties Matter Most for Waterproof Backpack Construction?
Selecting TPU coated nylon fabric requires a clear understanding of how the material will be used in the finished product. Waterproofness, tensile strength, tear resistance, abrasion resistance, and coating adhesion should be evaluated separately because each property addresses a different aspect of performance.
Waterproof Performance and Hydrostatic Resistance
A waterproof backpack fabric should resist water penetration under the conditions relevant to the product. The appropriate test method depends on the construction, intended exposure, and applicable product requirements.
Hydrostatic resistance testing can help assess the ability of a fabric to withstand water pressure. Results should be interpreted alongside coating integrity, sample preparation, and the test method used.
For a backpack designed for prolonged exposure to rain, the required material performance may differ from that of a travel bag intended mainly for occasional showers. Manufacturers should define the expected conditions before setting acceptance criteria.
The finished product also needs testing. Seams, closures, pockets, and attachment points can become leakage paths even when the main fabric panels perform well.
Abrasion Resistance in Contact with Rough Surfaces
Abrasion occurs when the material rubs against another surface. Backpack bottoms, side panels, and exposed corners are particularly likely to experience contact with rock, soil, equipment, and vehicle interiors.
A durable TPU coating can protect the underlying textile, but abrasion performance depends on the complete composite. Coating formulation, surface texture, thickness, and adhesion can all affect how the material responds to repeated rubbing.
Manufacturers should identify the areas most likely to wear and use representative test conditions when comparing candidate fabrics. A single abrasion result should not be used to predict the full service life of a backpack because real-world wear also depends on load, contact pressure, movement, and maintenance.
Tear Resistance and Puncture Resistance
Tearing and puncturing are different failure mechanisms. A tear can begin at a cut or damaged edge and propagate through the textile under tension. A puncture involves a concentrated force that penetrates the material.
Both properties may matter for expedition backpacks and equipment bags. A pack carrying climbing hardware, tools, or other rigid objects may encounter localized contact that places stress on the fabric surface.
The woven nylon substrate contributes to the composite’s resistance to mechanical damage, but performance varies with construction and material quality. Testing should reflect the intended product rather than relying solely on denier as a proxy for strength.
Design measures can also reduce damage. Reinforcing high-wear panels, protecting sharp contact areas, and avoiding unnecessary stress concentrations can improve the durability of the finished bag.
Coating Adhesion and Composite Integrity
The bond between the TPU layer and nylon substrate is another important consideration. A coating that separates from the textile may lose its protective function and create problems during fabrication or use.
Manufacturers should examine the surface for visible defects and evaluate adhesion using an agreed test method. Flexing, folding, and repeated handling can provide additional information about how the composite behaves under conditions similar to those encountered in production.
Storage and processing conditions should also be controlled. Excessive heat, contamination, or unsuitable handling may affect the material before it reaches the final assembly stage.
Why Does Double-Side TPU Coating Matter?
For certain outdoor products, manufacturers may consider double-side TPU coated nylon rather than a construction with only one coated surface. The choice depends on how the material is assembled and which surfaces require protection.
Double-side coating can provide TPU layers on both sides of the nylon substrate. This arrangement may be useful when both surfaces need a coated finish or when the product design requires specific joining and surface characteristics.
However, double-side coating does not automatically make a finished backpack waterproof or guarantee higher abrasion resistance. The results depend on coating thickness, formulation, adhesion, seam construction, and the exposure conditions of the finished product.
Surface Protection During Use
A backpack’s exterior is exposed to rain, dirt, and abrasion, while the interior may encounter damp equipment, condensation, or contact with stored items. A double-side construction allows designers to consider the characteristics of both surfaces when specifying the composite.
The precise benefit depends on the material configuration. Buyers should confirm which side is intended for the exterior, how the coated surfaces behave during assembly, and whether the fabric meets the product’s cleaning and maintenance requirements.
Compatibility with Joining Processes
TPU is a thermoplastic material, and suitable TPU surfaces can be joined using compatible welding processes. For some backpack designs, welding may help reduce the number of needle holes associated with conventional sewn seams.
The suitability of high-frequency welding depends on the specific TPU formulation and the complete composite structure. Fabric thickness, coating composition, electrode geometry, pressure, power, and cycle time can influence the result.
Manufacturers should conduct trial welds using the actual production material. They should inspect the resulting joint for continuity, distortion, damage, and leakage where waterproof performance is required.
Welding should not be assumed to be suitable for every panel or attachment point. Some constructions may require sewing, reinforcement, adhesives, or a combination of joining methods. The manufacturing process should be selected according to the structural and waterproof requirements of the finished product.
How Should Manufacturers Design Seams and Reinforced Areas?
The material specification is only one part of backpack durability. Pattern design and assembly determine how loads move through the finished product and where stress is concentrated.
Even strong TPU coated nylon fabric can fail prematurely if the bag design creates excessive stress around narrow seams, sharp corners, or poorly supported attachment points.
Reinforcing High-Load Areas
Shoulder strap anchors, grab handles, compression strap attachments, and the lower corners of a backpack may experience concentrated forces. These locations should be evaluated separately from large, relatively flat panels.
Reinforcement patches can distribute loads over a wider area when they are correctly designed and integrated into the structure. The reinforcement material and attachment method must be compatible with the main fabric and intended use.
Manufacturers should assess the complete assembly rather than testing only the fabric sample. Pull tests on representative strap and handle attachments can help identify weak points before production begins.
Managing Seam Geometry
Seam direction, width, overlap, and location can affect the finished bag’s mechanical performance and resistance to water ingress.
Corners and intersections deserve particular attention because several material layers may overlap or change direction. These areas can be more difficult to weld or seal consistently than straight sections.
Prototype testing helps reveal problems that are not apparent from a flat pattern. Manufacturers should examine seam appearance, alignment, local distortion, and leakage under representative conditions.
Where sewing is used, needle holes may require additional protection if the design demands a high level of water resistance. Where welding is used, the seam must be validated for both structural strength and the required degree of sealing.
Balancing Durability with Weight
Adding reinforcement can improve load distribution, but excessive reinforcement increases weight and may make the backpack less flexible. The objective is not to make every panel as heavy as possible; it is to place sufficient material where the expected loads and wear justify it.
A carefully selected combination of 420D and 840D constructions may be appropriate for certain products, with different fabrics used in different zones. Any such combination must account for differences in thickness, flexibility, joining behavior, and appearance.
Material zoning should be validated through prototype testing because the transition between fabrics can itself become a stress concentration.
What Quality Tests Should Buyers Request from a TPU Fabric Supplier?
A clear inspection plan helps buyers compare suppliers and reduces the risk of receiving material that does not match the approved specification.
Testing should cover both the raw composite and the processes used to manufacture the finished backpack. The exact requirements depend on the product’s design, intended market, and expected service conditions.
| Quality check | What it helps evaluate |
|---|---|
| Fabric thickness and mass | Consistency of the supplied composite |
| Zugfestigkeit | Resistance to pulling forces in specified directions |
| Reißfestigkeit | Resistance to tear propagation under the selected test method |
| Abriebfestigkeit | Response to repeated surface rubbing |
| Hydrostatische Beständigkeit | Resistance to water penetration under defined conditions |
| Coating adhesion | Bond integrity between TPU and nylon |
| Flexibilität bei niedrigen Temperaturen | Material behavior under specified cold conditions |
| Welding trials | Compatibility with the proposed joining process |
| Finished-bag testing | Performance of seams, closures, attachments, and panels together |
Test methods and acceptance limits should be agreed upon before production. Results from different methods or laboratories may not be directly comparable, so the test procedure should accompany the reported value.
Buyers should also ask whether the supplier can provide technical data sheets, sample rolls, batch identification, and relevant test documentation. These records make it easier to confirm that the material used in mass production matches the approved sample.
For critical applications, prototype testing should reproduce the loads, environmental exposure, and handling conditions expected during use. Laboratory measurements provide useful evidence, but the final bag must still be assessed as a complete product.
How Can Buyers Specify TPU Coated Nylon for Different Outdoor Products?
A useful material specification should describe the required performance rather than simply naming a fabric construction. Buyers should identify the intended application, expected loads, waterproof requirements, joining process, and acceptable finished-product weight.
The following considerations can help organize the selection process.
For lightweight hiking backpacks: Prioritize a suitable balance of composite weight, flexibility, abrasion resistance, and waterproof performance. Check whether the material can withstand expected contact with vegetation, rock, and packed equipment.
For expedition backpacks: Give particular attention to load-bearing areas, tear resistance, abrasion exposure, and the performance of strap and handle attachments. Reinforcement requirements should be assessed alongside the main fabric specification.
For waterproof duffel bags: Evaluate panel durability, base protection, closure design, and the sealing of seams and openings. The material must suit both the intended load and the bag’s handling conditions.
For specialized equipment bags: Consider the dimensions, weight, surface characteristics, and handling requirements of the items being carried. Sharp or rigid equipment may require additional protection in selected contact areas.
These categories are starting points, not fixed rules. A lightweight bag may still require substantial reinforcement, while a heavy-duty product may benefit from lighter fabric in areas that carry little load.
Working with a TPU Fabric Manufacturer
Material development is more effective when the fabric supplier understands the finished product rather than receiving only a request for a particular denier value.
Manufacturers should provide information about the bag’s intended use, required water resistance, expected load, target weight, panel dimensions, and proposed joining method. Sample evaluation can then focus on the properties most relevant to the application.
For products requiring double-side TPU coated nylon, buyers should confirm the coating arrangement, fabric construction, and available specifications. The 420D and 840D options offered for outdoor equipment provide starting points for evaluating different structural requirements, but the final choice should be based on the actual technical data and prototype results.
It is also useful to discuss customization early in development. Changes to fabric construction, coating configuration, color, or thickness can affect manufacturing behavior and should be reviewed before production settings are finalized.
A supplier capable of providing technical data, application guidance, and customized samples can help shorten the material evaluation process. Nevertheless, responsibility for validating the finished backpack remains with the product manufacturer.
Final Considerations for Waterproof Backpack Fabric Selection
Selecting TPU coated nylon fabric for outdoor backpacks requires a balanced assessment of water resistance, mechanical performance, weight, coating integrity, and manufacturing compatibility. Neither denier nor coating structure alone determines how a finished bag will perform.
420D and 840D nylon constructions can support different product design priorities, while double-side TPU coating may suit applications that require coated surfaces on both sides of the textile. The right combination depends on the expected load, wear conditions, construction method, and waterproof requirements.
Manufacturers should compare technical specifications, test representative samples, and validate the complete bag before approving a material for mass production. Attention to reinforced areas, seam design, coating adhesion, and finished-product testing helps ensure that the chosen composite is appropriate for its intended use.
For outdoor equipment brands developing waterproof backpacks, travel bags, and expedition duffels, TPU coated nylon provides a material option worth evaluating when waterproof protection and mechanical durability must be considered together. A specification-led selection process offers a more reliable basis for choosing the right fabric than relying on a single material rating.